 Preservatives(food)
 Flavors
 Acidulants
 Sweeteners
 Antioxidants
 Colorants(food)
 Nutraceutical Ingredients (food)
 Nutrient Supplements
 Emulsifiers
 Collectors
 Dust Suppressants
 Explosives and Blasting Agents
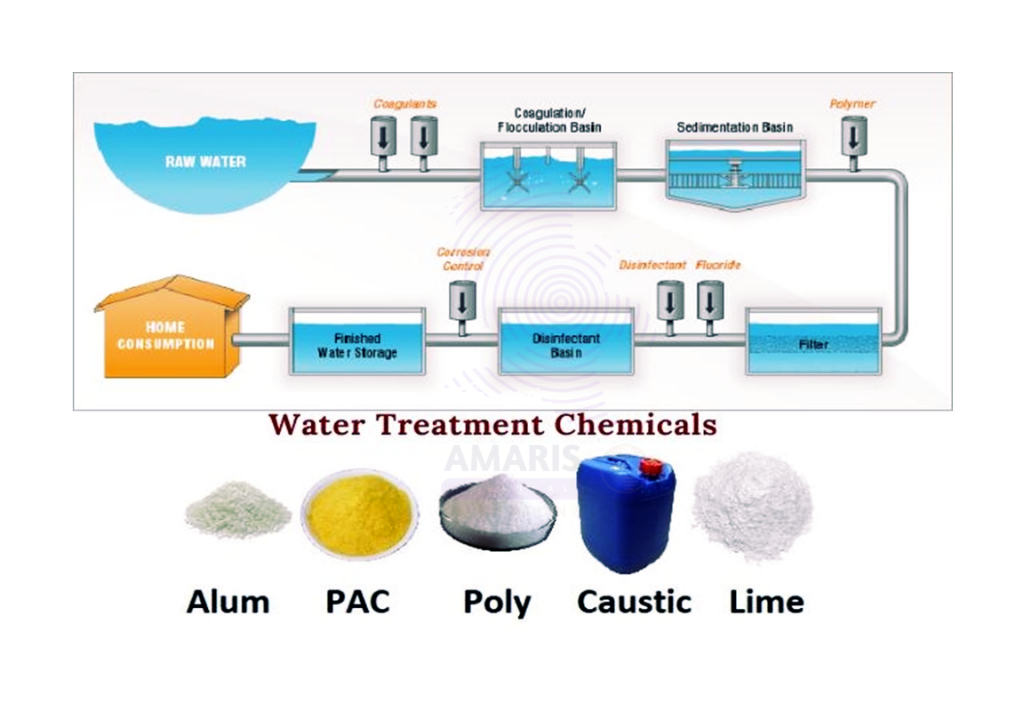
 Flocculants and Coagulants
 Frothers
 Leaching Agents
 pH Modifiers
 Precious Metal Extraction Agents
 Antioxidants(plastic)
 Colorants (Pigments, Dyes)
 Fillers and Reinforcements
 Flame Retardants
 Monomers
 Plasticizers
 Polymerization Initiators
 Stabilizers (UV, Heat)
 Antifoaming Agents
 Chelating Agents
 Coagulants and Flocculants
 Corrosion Inhibitors
 Disinfectants and Biocides
 Oxidizing Agents
 pH Adjusters
 Scale Inhibitors( water)
 Antioxidants(cosmetic)
 Emollients
 Oils
 Carrier Oills
 Essential Oils
 Humectants
 Preservatives
 Surfactants(cosmetic)
 Thickeners
 UV Filters
 Fragrance (Cosmetics)
 Fertilizers
 Soil Conditioners
 Plant Growth Regulators
 Animal Feed Additives
 Biostimulants
 Pesticides (Herbicides, Insecticides, Fungicides)
 Active Pharmaceutical Ingredients (APIs)
 Excipients
 Solvents(pharmaceutical)
 Antibiotics
 Antiseptics and Disinfectants
 Vaccine Adjuvants
 Nutraceutical Ingredients (pharmaceutical)
 Analgesics & Antipyretics
 Analytical Reagents
 Solvents(lab)
 Chromatography Chemicals
 Spectroscopy Reagents
 microbiology-and-cell-culture-reagents
 Molecular Biology Reagents
 Biochemical Reagents
 Inorganic and Organic Standards
 Laboratory Safety Chemicals
 Specialty Laboratory Chemicals(Special Laboratory Equipment)
 Demulsifiers
 Hydraulic Fracturing Fluids
 Scale Inhibitors(oil)
 Surfactants(oil)
 Drilling Fluids
 Dyes and Pigments
 Bleaching Agents
 Softening Agents
 Finishing Agents
 Antistatic Agents
 Admixtures
 Waterproofing Agents
 Sealants and Adhesives
 Curing Compounds
 Concrete Repair Chemicals
 Anti-Corrosion Coatings
 Surfactants(cleaning)
 Builders
 Enzymes
 Solvents (Cleaning)
 Electronic Chemicals
 Catalysts
 Lubricants
 Photographic Chemicals
 Refrigerants
 Automotive chemicals
 Pyrotechnic Chemicals
 Biodegradable Surfactants
 Bio-based Solvents
 Renewable Polymers
 Carbon Capture Chemicals
 Wastewater Treatment Chemicals
 Pigments
 Solvents(paint)
 Specialty Coatings
 Binders/Resins
 Additives
 Driers
 Anti-Corrosion Agents
 Functional Coatings
 Application-Specific Coatings
 Leavening Agents
 Dough Conditioners
 Flour Treatments
 Fat Replacers
 Decoratives
 Preservatives(baking)
 Plasticizers & Softeners
 Reinforcing Agents
 Adhesion Promoters
 Vulcanizing Agents
 Antidegradants
 Blowing Agents
 Fillers & Extenders
 Accelerators & Retarders
From Laboratory to Factory: How Chemical Testing Supports Product Quality 🔬🏭

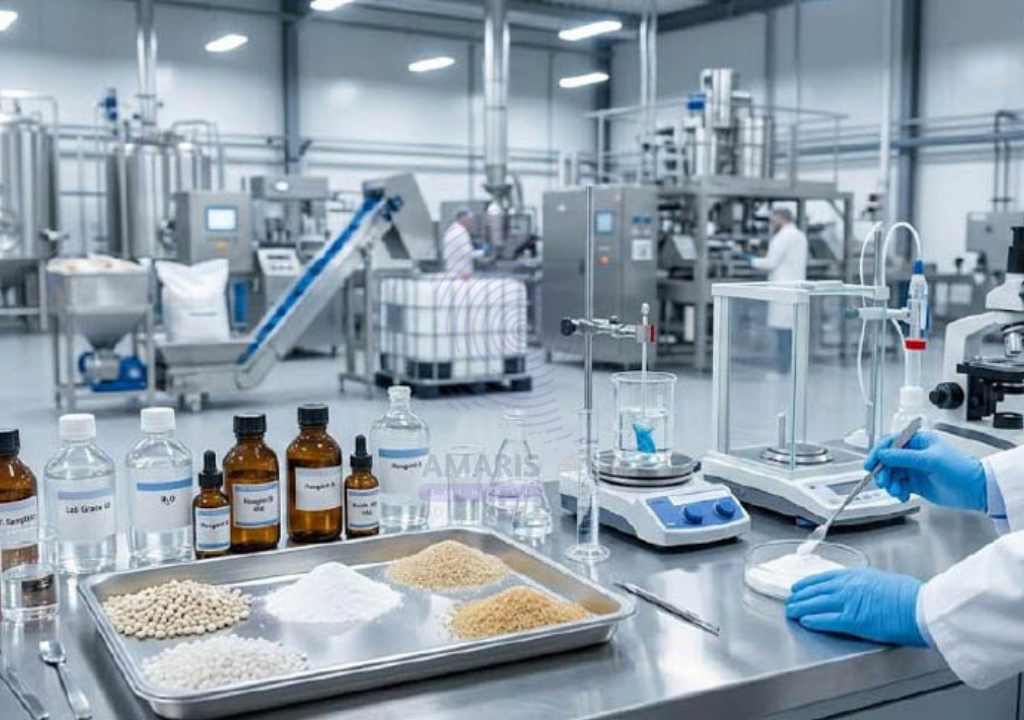
Every manufactured product begins with raw materials, but how can businesses ensure those materials meet the required standards? From paints and detergents to cosmetics, food ingredients, construction materials, and industrial chemicals, chemical testing plays a vital role in ensuring product quality, consistency, and reliability.
Laboratory analysis helps manufacturers understand the composition and properties of their materials before they enter production. By connecting laboratory results with factory operations, businesses can reduce defects, improve efficiency, and deliver products that meet customer expectations.
Why Is Chemical Testing Important?
Raw materials can vary in purity, concentration, moisture content, and other properties. Even small variations may influence the final product, particularly when precise formulations are required.
Chemical testing helps manufacturers verify whether incoming materials meet their specifications. It can also identify impurities, detect inconsistencies, and provide information needed to determine whether a material is suitable for its intended application.
For example, a manufacturer producing cleaning products may need to verify the concentration of a key ingredient, while a paint manufacturer may evaluate pigment properties to support consistent colour and coverage.
The Role of Laboratory Analysis 🔬
Laboratories use different analytical techniques depending on the substance being tested and the information required.
Methods such as pH measurement, titration, moisture analysis, spectroscopy, and chromatography can help determine chemical properties, concentrations, or the presence of particular components.
The choice of method depends on the material, the required accuracy, and the applicable testing standards. Instruments must also be maintained appropriately, and testing procedures should be validated or verified for their intended purpose.
Reliable results give manufacturers a stronger basis for making decisions about raw materials, formulations, and production processes.
Connecting Laboratory Results to Factory Production
Laboratory testing is most valuable when its findings inform actual manufacturing decisions.
Before production begins, incoming raw materials may be checked against approved specifications. During production, samples can be tested to confirm that important parameters remain within defined limits. Finished products can then undergo final quality checks before release.
This approach helps identify potential problems at different stages rather than waiting until a customer reports a defect.
For example, if a batch of detergent does not meet its required pH specification, timely testing can help quality teams investigate the formulation, raw materials, or process conditions responsible.
Preventing Defects and Reducing Waste
Poor-quality raw materials and uncontrolled production conditions can result in rejected batches, reprocessing, wasted ingredients, and delayed deliveries.
Early detection is often more efficient than correcting a problem after manufacturing is complete. Regular testing allows manufacturers to identify deviations sooner and investigate their causes.
Over time, analysing test results across multiple batches can also reveal recurring patterns. Businesses may use this information to improve supplier selection, adjust quality controls, and make production more consistent.
Chemical Testing and Regulatory Compliance
Many industries operate under specific quality, safety, and regulatory requirements. Pharmaceutical products, food ingredients, cosmetics, laboratory reagents, and construction materials may each require different testing approaches and documentation.
Manufacturers should maintain appropriate specifications, test reports, batch records, and certificates of analysis where applicable. Testing must follow relevant standards and regulatory requirements, and results should be reviewed by competent personnel.
It is also important to remember that a single laboratory test does not automatically establish that a product is safe or compliant. Appropriate assessment may require several tests, documented procedures, and additional quality checks.
The Value of Reliable Laboratory Chemicals
Accurate testing depends not only on instruments and skilled personnel but also on suitable laboratory reagents, reference materials, solvents, and other supplies.
Using materials that meet the required grade and specifications helps reduce the risk of introducing impurities or measurement errors. Proper storage, handling, and documentation are equally important in maintaining the reliability of laboratory work.
As manufacturers increasingly rely on data to guide production decisions, dependable laboratory supplies remain an important part of effective quality management. 🧪
Building Better Products Through Science
Chemical testing connects scientific analysis with practical manufacturing. It helps businesses understand their raw materials, monitor production, investigate defects, and verify finished-product quality.
For Kenya’s growing manufacturing sector, investing in reliable laboratory testing and effective quality-control systems can support greater consistency, less waste, and stronger customer confidence.
Ultimately, quality does not begin at the end of the production line—it begins with understanding the materials that go into every product. 🔬🏭